High-Efficiency 195-Pint Portable Dehumidifier for Commercial and Industrial Humidity Control with Integrated Condensate Pump
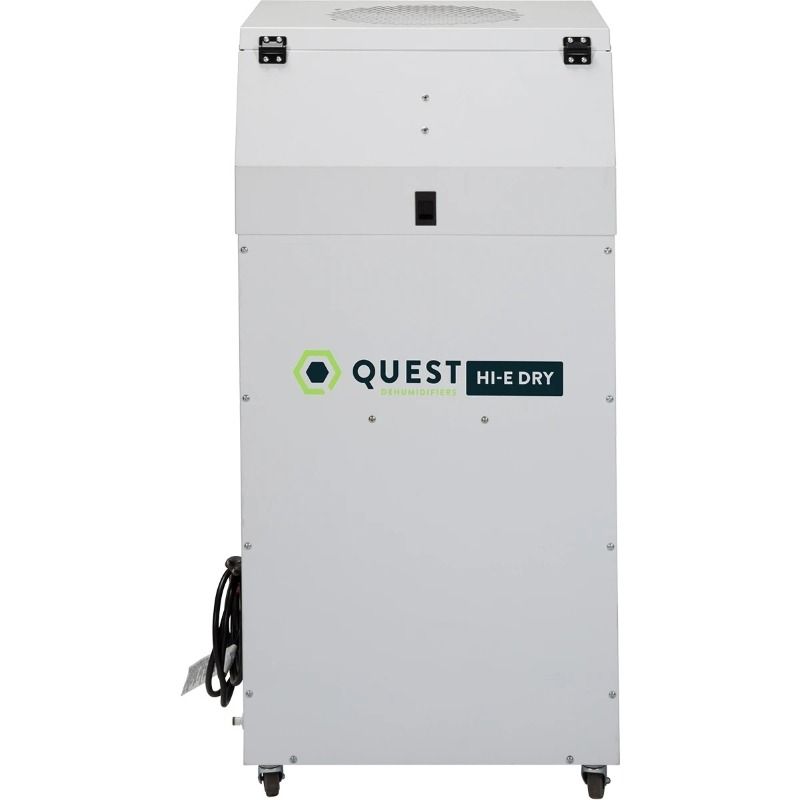
The Quest Hi-E Dry 195 (Model 4046400, SKU HI7908) is a high-capacity portable dehumidifier designed to provide efficient moisture removal and reliable humidity control for commercial and industrial environments. Delivering up to 195 pints of moisture removal per day at 80°F and 60% relative humidity, this self-contained refrigerant dehumidification system combines energy-efficient performance with a portable design, onboard digital controls, MERV-11 air filtration, and an integrated condensate pump. Four casters and a 10-foot power cord provide flexible placement and convenient relocation between work areas, while the included 30-foot drain hose supports continuous condensate removal.
Key Benefits
- High-Capacity Dehumidification Performance – Removes up to 195 pints of moisture per day at 80°F and 60% relative humidity to help control elevated humidity levels in demanding commercial environments.
- Energy-Efficient Moisture Removal – Delivers a rated efficiency of 6.1 pints per kilowatt-hour at 80°F and 60% relative humidity to support effective moisture control with measured energy consumption.
- Portable Four-Caster Design – Allows the unit to be moved between work areas as humidity-control requirements change.
- High-Volume Airflow – Provides 610 CFM of airflow to circulate air through the dehumidification system.
- Flexible Placement – Features a self-contained design, a 10-foot power cord, and a portable cabinet for convenient deployment without requiring a permanent HVAC installation.
- Integrated Condensate Pump – Includes a 30-foot drain hose and a pump capable of lifting condensate up to 17 feet to support flexible drainage arrangements.
- Onboard Digital Humidity Controls – Provides integrated controls for convenient operation and humidity management.
- MERV-11 Air Filtration – Uses a nominal MERV-11 filter to capture airborne particles as air passes through the dehumidifier.
High-Capacity Dehumidification Performance
The Quest Hi-E Dry 195 provides up to 195 pints per day of moisture removal at 80°F and 60% relative humidity, with a rated efficiency of 6.1 pints per kilowatt-hour and an energy factor of 2.9 liters per kilowatt-hour under the same conditions. At 75°F and 50% relative humidity, the unit removes up to 145 pints per day, with a rated efficiency of 4.7 pints per kilowatt-hour and an energy factor of 2.2 liters per kilowatt-hour. Its operating temperature range of 56°F to 95°F supports humidity management in suitable commercial and industrial environments.
Humidity Control and Moisture Removal
The Quest Hi-E Dry 195 uses refrigerant-based dehumidification to remove excess moisture from the air and help maintain appropriate humidity levels in commercial spaces. Its onboard digital dehumidistat provides integrated humidity control, while the unit's automatic restart feature restores its previous operating settings following a power interruption. The system uses R454B refrigerant and is designed to operate within a specified ambient temperature range of 56°F to 95°F.
Airflow and Distribution
The Quest Hi-E Dry 195 delivers 610 cubic feet per minute (CFM) of airflow at the manufacturer's specified test conditions. This airflow circulates humid air through the dehumidification system to support moisture removal throughout the intended space. A nominal MERV-11 air filter measuring 16 inches by 20 inches by 2 inches provides filtration of airborne particles entering the unit. The filter should be inspected and maintained in accordance with the manufacturer's instructions to support proper airflow and system performance.
Portable and Flexible Installation
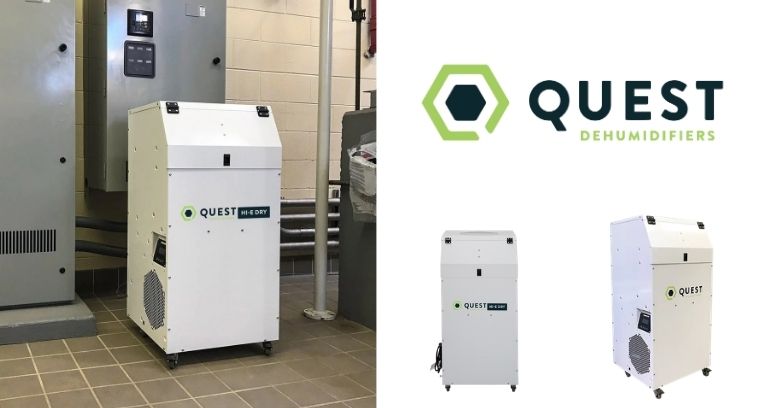
The self-contained portable design allows the Quest Hi-E Dry 195 to be positioned where supplemental moisture control is needed without requiring a permanent HVAC installation. Four caster wheels facilitate movement between suitable work areas, while the 10-foot power cord provides additional placement flexibility. The unit measures approximately 19 inches long by 20 inches wide by 42 inches high and weighs 130 pounds. Its compact cabinet footprint supports deployment in a variety of commercial and industrial environments, subject to the manufacturer's installation, clearance, and operating requirements.
Condensate Management
The Quest Hi-E Dry 195 incorporates an internal condensate pump to remove water collected during dehumidification. The unit includes a 30-foot drain hose with a 1/4-inch inside diameter, and the pump can lift condensate up to 17 feet. This integrated condensate management system supports flexible drainage routing and reduces the need for manual water removal. The drain hose must be routed and installed according to the manufacturer's instructions to ensure reliable drainage and prevent water leakage.
Controls, Humidity Management and Electrical Connection
The Quest Hi-E Dry 195 features onboard digital controls and an integrated dehumidistat for humidity management. Its automatic restart function restores the previous operating settings after a power interruption. The unit operates on a 110–120 VAC, single-phase, 60 Hz power supply and draws approximately 12 amps at the manufacturer's specified test conditions of 80°F and 60% relative humidity. It is equipped with a 14-gauge, 10-foot power cord terminating in a NEMA 5-20P plug. The manufacturer specifies a dedicated 20-amp circuit. Installation must comply with the manufacturer's electrical requirements and applicable local codes.
Commercial and Industrial Applications
The Quest Hi-E Dry 195 is designed for professional moisture-control applications where portable, high-capacity dehumidification is required. Suitable applications may include commercial facilities, indoor agriculture, storage areas, workshops, construction environments, and other spaces requiring supplemental humidity management within the unit's specified operating range. Its 195-pint-per-day moisture removal capacity, 610 CFM airflow, onboard digital controls, MERV-11 filtration, and integrated condensate pump make it suitable for applications requiring substantial moisture removal and flexible equipment placement. Actual performance depends on ambient temperature, relative humidity, moisture load, and installation conditions.
Mobility and Deployment
The Quest Hi-E Dry 195 features a portable cabinet with four casters for relocation between suitable work areas. Its 130-pound operating weight, compact dimensions, and 10-foot power cord support flexible deployment where moisture-control needs may change. The included condensate pump and 30-foot drain hose further support placement flexibility by allowing condensate to be discharged at a suitable drainage location within the pump's specified lift capability.
Service and Maintenance
The Quest Hi-E Dry 195 incorporates a replaceable air filtration system and onboard controls to support routine operation and maintenance. The nominal MERV-11 filter measures 16 inches by 20 inches by 2 inches and should be inspected and serviced according to the manufacturer's maintenance instructions. Routine maintenance should also include inspection of the condensate drain hose, pump drainage path, and accessible components as directed in the owner's manual. Maintaining clean filtration and unobstructed condensate drainage helps support reliable operation and sustained dehumidification performance.
Warranty
The Quest Hi-E Dry 195 is covered by a five-year limited manufacturer's warranty. Warranty coverage is subject to the manufacturer's applicable terms, conditions, exclusions, and requirements. Refer to the official Quest warranty documentation for details concerning coverage, registration, installation, and service requirements.
Recommended Accessories
- Replacement MERV-11 Air Filter – Nominal 16-inch by 20-inch by 2-inch filter; confirm the compatible replacement part number with Quest.
- Condensate Drain Hose – The unit includes a 30-foot drain hose with a 1/4-inch inside diameter.
- Condensate Pump – An internal condensate pump is included with the unit; confirm compatibility with the manufacturer before selecting replacement components.
- Additional Ducting or Air Distribution Accessories – Confirm compatibility and approved configurations with Quest before selecting accessories.
High-Capacity Moisture Control with the Quest Hi-E Dry 195
Experience flexible, high-capacity humidity control with the Quest Hi-E Dry 195 portable dehumidifier. Combining moisture removal of up to 195 pints per day at 80°F and 60% relative humidity with onboard digital controls, MERV-11 air filtration, four-caster mobility, and an integrated condensate pump, this commercial-grade dehumidification system provides targeted moisture management for suitable commercial and industrial applications.